Top China Plastic Prototyping Service Factory for Rapid Custom Prototypes
2026-10-07
You don’t need another Chinese supplier that promises fast and delivers a box of warped ABS two weeks late. You need a factory that treats rapid custom prototypes as the main event, not an afterthought. That’s the exact position ProtoMat holds in China’s plastic prototyping scene. In the sections ahead, we’ll show what actually separates top-tier prototyping services from the noise—and how to spot the difference before you pay.
Inside a Prototyping Floor Built for Speed
The first thing you notice is how the floor resists any kind of waiting. Benches are arranged not by department but by sequence of operations—cutting, soldering, assembly, testing—so a prototype can move from raw stock to loaded firmware in under an hour. There’s no central storage room; instead, every tool and fastener lives in rolling carts that follow the current project.
Speed here comes from deliberate constraint. The supplies are limited to a curated set of motors, boards, sensors, and structural profiles that most teams actually use. That sounds restrictive until you watch someone build: with fewer choices, decisions get made in seconds, and the components are already known to work together. The floor manager calls it “controlled impatience.”
What makes it genuinely fast isn’t just equipment—it’s permission. Engineers and designers on the floor can cut material, modify fixtures, and run destructive tests without filling out a request or waiting for a specialist. Every bench has a small set of wrenches, a heat gun, and a bin of labeled fasteners. The result is that an idea gets physically tested in the time it takes to explain it.
Plastic Selection Beyond the Datasheet
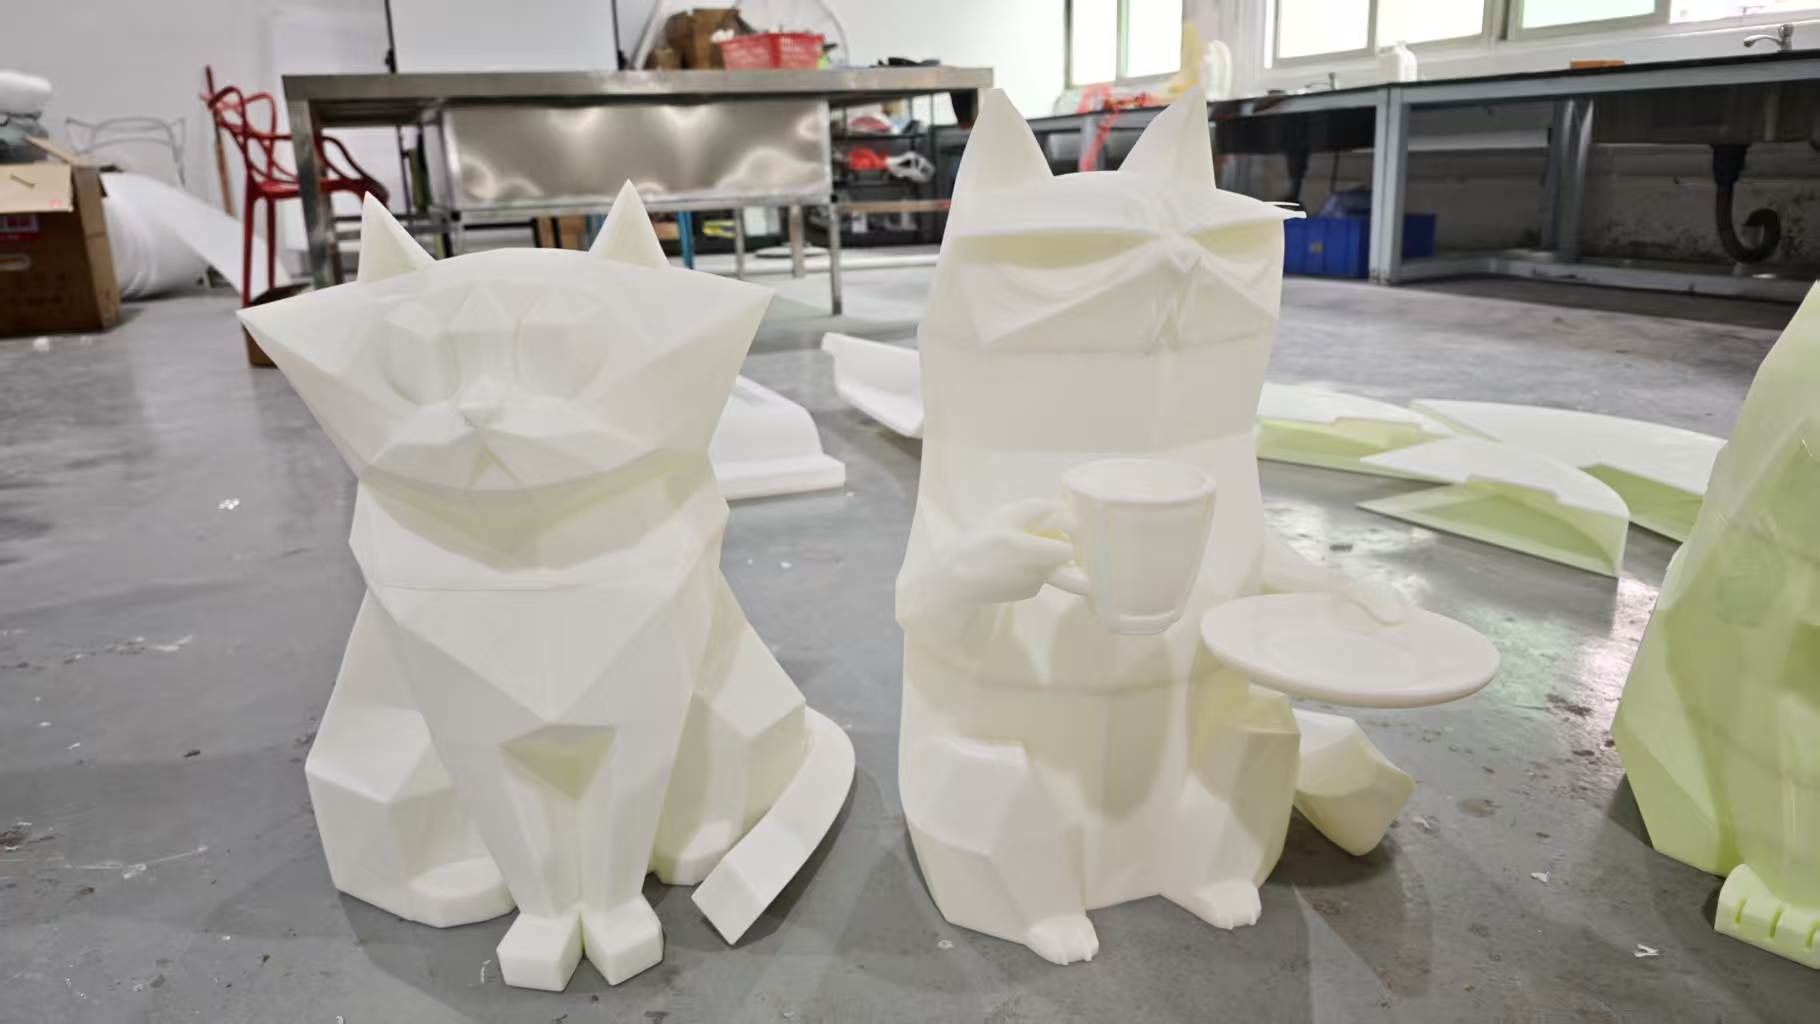
The datasheet rarely tells you how a resin behaves after six months in warm transmission fluid, or whether it will survive a cold snap with a sharp notch. Numbers like tensile strength and HDT are captured on clean, standardized specimens, yet real parts carry knit lines, weld lines, molded-in stress, and uneven crystallinity. A material that looks superb on paper can crack in the field simply because the gate froze too early or a radius was machined a little too sharp.
Talking to processors, toolmakers, and field engineers often uncovers what the spec sheet omits. Ask for actual snap-fit trials, chemical exposure coupons, or parts pulled from a 500-hour thermal aging oven. Compare lot-to-lot melt flow stability if you are molding thin walls, and watch for additive blooming or viscosity shifts during regrind. The final choice is not the highest tensile number; it is the material that tolerates your process window, your assembly loads, and your end-use abuse without surprises.
When Tolerances Decide Your Product’s Fate
Tolerances look like boring numbers on a drawing, but they quietly separate a product that feels premium from one that rattles apart. A phone screen that sits a few microns too proud of its frame makes the whole device feel cheap. Inside an engine, a piston clearance that drifts by less than the width of a human hair can mean the difference between smooth power delivery and a seized block. These are not abstract engineering concerns—they are the physical reality of every part that has ever been mass-produced.
The trouble is that tolerances rarely fail alone. A shaft that is slightly undersized meets a bore that is slightly oversized, and the resulting slop multiplies through the assembly until a hinge wobbles or a connector loosens. Designers often treat tolerance stacks as a final check, but in practice they are the first thing to bite when suppliers change tooling or a new batch of raw material behaves differently. Products do not usually die from a single bad dimension; they die from the accumulated drift that no one measured until customers started complaining.
Seasoned engineers learn to read tolerances like a dialect: some dimensions can breathe, others must be held ruthlessly tight, and knowing which is which is what keeps a product alive on the line. A tolerance note is not just a limit—it is a bet on how much variation the design can absorb before the user notices. When that bet is wrong, the product's fate is sealed long before the first shipment leaves the factory.
From Single Iterations to Pilot Batches Without a Hitch
Scaling from a lone prototype to a pilot run usually exposes all the assumptions nobody wrote down. Small tweaks that took five minutes by hand turn into an hour of fixture wrestling when you need fifty units by Thursday. The trick is to treat that first iteration not as a finished thing but as a set of repeatable notes—tool paths, torque settings, supplier lead times, even the order of assembly.
What saves time later is running a pre-pilot with the exact materials and machines planned for the batch, not the convenient ones sitting on the bench. A single iteration hides variance because you nurse it through each step. A pilot batch needs parts that fit without coaxing, cycles that don't drift after lunch, and operators who can swap in without a twenty-minute explanation.
Bottlenecks tend to show up in the quietest places: labeling, packaging, test fixture changeover. If those aren't given the same attention as the headline process, the pilot stalls on tedious fixes. Build the pilot plan around those unglamorous tasks and the jump from one unit to a hundred stays boring—and boring is exactly what you want.
Cosmetic Finishes That Make Reviewers Ask for Production
There’s a particular kind of finish that stops a reviewer mid-swipe, makes them zoom into the photo, and then flood the comments asking if the brand plans to release it. A liquid highlighter from a recent press kit did exactly that—it had a pearl suspension so fine it vanished in direct sunlight but turned into a soft, wet-look veil under bathroom lighting. People described the glow as real skin moisture rather than glitter, and some joked they would ration the sample for special occasions only.
The same pattern showed up with a blurring primer that felt more like a silky serum than a silicone mask. It didn’t erase texture the way heavy powders do; instead, it diffused pores and redness while letting natural skin movement show through. Reviewers started tagging the brand daily, demanding a standalone launch, and one tester posted a side-by-side photo of their bare face and primed face. The difference was subtle enough to be believable but dramatic enough to convert half the comment section.
Lip products with a cream-to-powder shift triggered a similar response. The texture glided on with zero drag, set down to a blurred matte that somehow kept a hint of dimension, and didn’t crumble after hours. People who tried the trial size immediately asked where to buy the full version, and when the brand stayed quiet, fan-made swatch threads turned into mini campaigns. The common thread is that these finishes solve a specific complaint—greasy highlight, mask-like primer, drying lip color—without sacrificing the feel of bare skin, and that’s what makes reviewers feel like they’ve discovered something worth producing.
Working Across Time Zones With a Shenzhen-Based Team
When your engineering team is based in Shenzhen while product and design sit in North America, the usual 9-to-5 rhythm disappears almost immediately. Most of my calls with the Shenzhen crew happen either before 8 a.m. my time or after 9 p.m., because that’s when their workday is either winding down or just getting started. Instead of fighting that gap, we’ve built a routine around two short daily overlaps: one for handoff questions and one for demos. The rest of the day runs on written updates, recorded walkthroughs, and a shared decision log that anyone can read without waiting for a reply.
What surprised me most was how much clarity comes from not being able to talk in real time all day. A question that might have been a quick Slack ping now has to be written with enough context to be answered hours later, which forces everyone to think through edge cases before asking. We also treat the overlap window as sacred: no status meetings, only blocking issues and design reviews. That discipline keeps the asynchronous hours calm and keeps Shenzhen engineers from feeling like they’re always on call. Over time, the time zone difference stopped being a constraint and became the reason our documentation, code review, and release notes are far better than they were when we all sat in one office.
FAQ
Look beyond the glossy claims. A dependable factory will walk you through material options, show real photos of past work, and quote realistic lead times rather than promising the impossible.
For simple parts with standard materials, a seasoned shop can often deliver CNC-machined or 3D-printed prototypes within 3–7 days. Complex geometries, multi-cavity molds, or secondary finishes will extend that to two or three weeks.
Most established factories stock ABS, PC, nylon, PMMA, POM, and PEEK, plus softer options like TPU. If you need something uncommon, they can usually source it, but that may add a few days.
Yes, many Chinese prototyping services bridge the gap between one-off samples and pilot runs of a few hundred pieces. They often use vacuum casting or rapid injection molding for small batches.
Request first-article inspection reports, dimensional checks, and clear photos or video of the actual parts. A transparent factory won't hesitate to share these.
Reputable factories are used to signing NDAs and keeping customer files secure. Still, it's wise to share only what's necessary and mark drawings clearly.
You can usually specify painting, screen printing, laser engraving, texture, or polishing. Some shops also offer vapor smoothing for 3D-printed parts to get a smoother surface.
Many top-tier Chinese prototyping factories have English-speaking project managers and engineers. Clear drawings with notes, plus a short call, usually prevent most misunderstandings.
Conclusion
The factory floor moves at a pace that feels closer to a pit crew than a typical prototyping lab. Machines are arranged to minimize handling, and the team keeps tooling changes short, so a CAD file sent in the morning often becomes a physical part by the next day. But speed alone is not what sets this Shenzhen operation apart. Material selection goes well beyond comparing numbers on a datasheet — the engineers regularly pull from a curated range of filled nylons, polycarbonates, and soft-touch elastomers, and they are not shy about suggesting a resin that better matches your actual impact, heat, or wear conditions. That practical judgment matters, especially when tight tolerances on snap fits, living hinges, or threaded bosses make the difference between a part that assembles cleanly and one that needs rework.
Small design changes do not slow things down here. The same floor handles single revised iterations and pilot batches of a few hundred without retooling chaos, which keeps the transition from prototype to trial run remarkably smooth. When it comes to surface finish, the team treats texture, gloss, and color matching as part of the functional design, not an afterthought — samples arrive with SPI finishes, soft-touch coatings, or masked paint that often get mistaken for production parts during design reviews. Coordination is also built around your clock. A Shenzhen-based project contact stays responsive through overlapping hours, sends photo and video updates without being asked, and keeps a shared log of changes. It feels less like outsourcing and more like having an extension of your own product team, just one that can cut plastic the same day you approve the file.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/