High-Quality Prefabricated Fence Molds: Key Features for Long-Lasting Concrete Fences
2026-09-26
In the world of concrete fencing, the difference between a fence that stands for decades and one that crumbles within years often comes down to a single, overlooked factor: the mold. High-quality prefabricated fence molds are not just metal forms—they are the blueprint for durability, precision, and aesthetic appeal. With LugongMachinery, you’re not just buying molds; you’re investing in a system engineered to deliver long-lasting concrete fences, pour after pour. But what exactly separates a mediocre mold from a masterpiece? Let’s explore the key features that make all the difference.
Mold Materials That Survive Daily Concrete Pours
Concrete casting on a daily schedule eats through weak molds fast. The materials that actually hold up share two traits: they release cleanly without tearing, and they resist the abrasive paste that grinds down softer surfaces. Urethane rubber sits at the top of that list. A well-formulated polyurethane mold keeps its edges crisp pour after pour, flexing just enough to pop out intricate details without cracking. Unlike cheaper silicones that turn gummy after a week of wet curing, urethane stays firm and keeps dimensional stability even when the concrete generates heat during hydration.
For simpler shapes and high-volume work, ABS plastic and fiberglass-reinforced composites are the quiet workhorses. They take a beating from trowels, vibrating tables, and demolding hammers without warping. Steel molds earn their keep when you need thousands of identical pulls from the same form — the initial cost stings, but the surface finish stays glass-smooth years later. What surprises most people is that plain melamine-coated particleboard can survive dozens of pours if you seal the edges properly and avoid letting wet concrete sit overnight. The real difference isn't just the material itself; it's the release agent routine and how quickly you clean the mold after each pour. Neglect that, and even the toughest polyurethane will start pitting around the fine details.
Precision Joints That Cut Finishing Time
Most woodworkers know the frustration of sanding away hours on a joint that just won't sit flush. The difference comes down to how the mating surfaces are cut from the start. When every shoulder and cheek is machined to exact tolerances, the pieces lock together without visible gaps or misalignment. That means less filler, less scraping, and a finish-ready surface almost immediately after glue-up.
Our approach relies on carefully tuned joinery systems that produce repeatable, snug fits. Instead of relying on hand-tuning each connection, the cutting process itself accounts for wood movement and adhesive thickness. The result is a joint that closes tightly under moderate clamp pressure, leaving only a whisper-thin glue line. No more digging dried squeeze-out out of corners or re-cutting a tenon that shrank overnight.
For production shops, this translates directly into lower labor costs. A cabinet door frame that assembles clean on the first pass doesn't need a second trip to the bench. Edge joints in tabletops come off the clamps flat enough to skip the belt sander entirely. The time saved isn't theoretical; it shows up on the shop floor as fewer abrasive belts, quieter sanding stations, and a stack of parts that moves straight to finishing.
Reinforcement Guides Built Into the Mold
The idea of molding reinforcement guides directly into the tooling changes how inserts and stiffening ribs are positioned during each cycle. Instead of relying on separate jigs or manual alignment steps, the mold itself carries dedicated channels and shoulders that hold reinforcements in the exact place before plastic is injected. This removes a lot of the guesswork and makes setup faster on the floor.
Because those guide features are cut or EDM'd into the steel, they don't drift between shots. Every part sees the same contact faces, so rib placement stays consistent from the first cavity fill to the last. That repeatability matters when wall thicknesses are tight or when the reinforcement has to line up with mating components later in assembly. It also reduces the chance of flash or short shots around the insert, since there's less movement as material enters.
One overlooked benefit is how these built-in guides affect mold maintenance. If a guide surface begins to wear, it can often be touched up or replaced as part of a standard insert rather than rebuilding an entire alignment fixture. For high-volume work in automotive brackets or appliance housings, that's a practical difference. The design works best when mold makers plan the guide dimensions alongside ejection and cooling, so the reinforcement stays put without fighting the rest of the tool.
Surface Treatments That Make Demolding Effortless
Mold release problems rarely come from the part geometry alone—they often trace back to how the steel surface interacts with the resin or metal being formed. A well-chosen surface treatment lowers the surface energy enough to break the adhesive bond without sacrificing dimensional accuracy. Instead of relying on spray release agents that build up in vents and ribs, many shops now turn to low-friction coatings that stay put for thousands of cycles.
Among the options, PTFE-infused electroless nickel stands out because it combines corrosion protection with a slippery, non-stick finish that works on complex cores and slides. Diamond-like carbon (DLC) coatings take a different route: they are extremely hard and reduce galling on ejector pins and moving components, so the part pops free with less force. For high-temperature molding, ceramic or titanium nitride layers prevent the molten material from wetting the mold surface, which is often the hidden cause of sticking.
The payoff shows up in cycle time and tool maintenance. When the mold surface does not grab the part, operators can reduce ejector pressure, avoid stress whitening or cracking on delicate features, and skip frequent reapplication of release agents. Over a production run, that translates into fewer shutdowns for cleaning and polishing—making the treatment less of an add-on and more of a baseline requirement for trouble-free demolding.
Structural Bracing That Keeps Panels Flat Over Time
A well-designed bracing layout does more than stiffen the panel on day one. It distributes internal stress across the entire surface, so seasonal moisture swings and temperature cycles don't concentrate force at the edges or corners. Over time, that balanced load path is what stops a panel from cupping, twisting, or developing a visible bow in the middle.
Instead of relying on a single center rib or thick perimeter frame, the support pattern works in two directions. Short diagonal members intersect the main rails, creating small triangular zones that resist movement without adding much weight. This approach keeps the face sheet stable even when one side is exposed to direct sun or a damp wall cavity while the other side stays dry.
The hardware also plays a role. Fasteners with a slight shoulder allow the panel to expand and contract in place, while the bracing holds its overall shape. The result is a flat surface that stays flat through years of use—not because the material is stiff, but because the structure behind it manages movement in a controlled way.
Inspection Points That Reveal a Mold’s True Lifespan
The first sign is usually at the parting line. When a mold is new, the flash is either nonexistent or a hairline that wipes away with a fingertip. As the tool ages, you'll start seeing a thicker, uneven flash along the same edges, especially near the gate or deep ribs. That tells you the steel faces are no longer locking up as tightly as they once did, which often points to wear on the shutoffs or localized hobbing from repeated clamp pressure.
Another reliable checkpoint is dimensional drift on a known feature. If you've been tracking a critical boss diameter or a snap-fit length and it's moved by more than a few tenths even after process adjustments, the cavity or core insert has likely worn past its comfortable tolerance band. Surface finish is just as telling: a polished cosmetic face that starts showing micro-pitting or a dull gray haze usually means the coating is gone and the base steel is beginning to erode.
Don't ignore how the parts eject. Sticking, hanging up, or ejector pin marks that suddenly become deeper than normal often mean the draft angles have been compromised by wear, or the pins themselves are bell-mouthed in their bores. Pull the last three preventive maintenance reports and compare cycle counts to what was predicted. If the tool is consuming more downtime for flash removal, vent cleaning, or insert replacement than the original lifespan curve suggested, the real end of useful life is closer than the nominal shot count implies.
FAQ
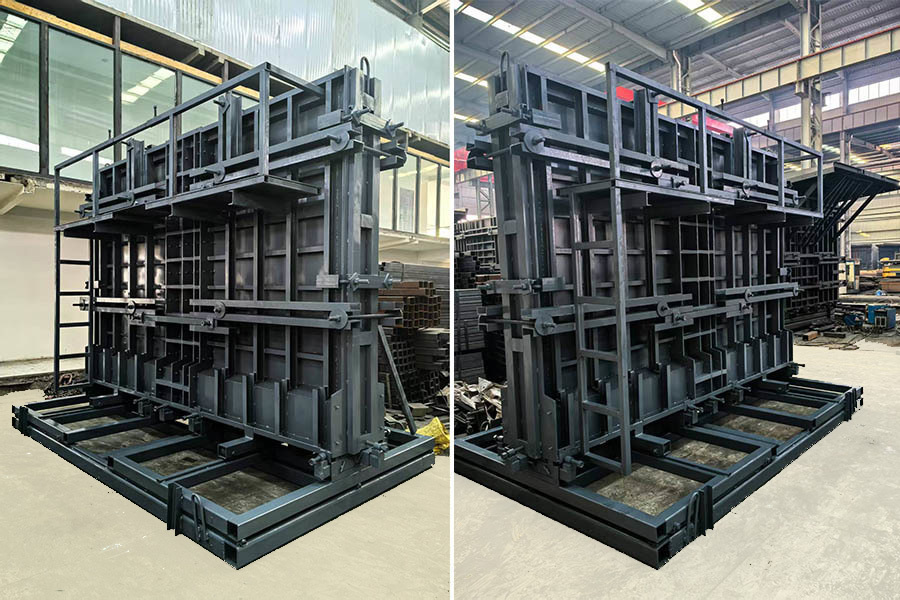
The mold needs to be built from heavy-duty steel with precise dimensional tolerances. If the panels come out with consistent thickness and sharp edges, the cured concrete resists cracking, moisture intrusion, and freeze-thaw cycles far better than hand-poured alternatives.
Well-planned rib patterns and reinforcement channels let you embed steel bars without guesswork. That internal structure, combined with uniform wall thickness from the mold, gives the panel the bending and impact resistance that keeps it standing through storms and ground shifts.
A smooth, non-porous mold face reduces water retention on the finished panel. Less surface water means less spalling and staining over time. Some molds also include subtle textures that hide micro-cracks while maintaining a clean architectural look.
Prefabricated molds eliminate warping, seam misalignment, and inconsistent panel dimensions. You get repeatable results, faster pouring cycles, and fewer rejected pieces, which adds up to lower labor costs and a fence line that looks uniform from end to end.
After every few pours, clean the mold faces with a non-abrasive scraper and apply a light release agent. Check hinge pins and locking clamps for play. Storing molds indoors or under a tarp prevents rust, which is the main cause of surface defects later.
Most well-engineered steel molds tolerate a range of mixes, from standard 4,000 psi concrete to fiber-reinforced and lightweight aggregates. The key is adjusting vibration time and release agent type to match the mix’s flow characteristics and early strength gain.
When every panel is the same length, height, and post-pocket position, installers can set posts and slide panels without field trimming or shimming. That precision shortens the installation schedule and prevents gaps or uneven joints that collect debris and weaken the fence over time.
Conclusion
A fence mold only earns its keep when it can shrug off daily pours without warping, chipping, or binding. The best ones use hardened alloy steels or heavy-gauge aluminum matched to the abrasive nature of wet concrete, not just any sheet metal. Look for precision-machined joints that close tight enough to eliminate flash and cut grinding time after each panel cures. Built-in guides for rebar or mesh mean less fiddling with spacers, so reinforcement sits exactly where it belongs for crack control. Surface treatments matter more than they get credit for: a low-friction coating or polished contact face lets you strip forms in seconds instead of wrestling with a stuck panel.
Over years of service, the difference becomes structural. Molds with cross-bracing and stiffened side rails keep long panels from bowing, which is what ruins the straight sightlines of a fence line. The hidden quality indicator is the inspection point—threaded inserts, wear plates, and hinge areas that show how many cycles a mold has actually handled. A mold that looks clean but has sloppy pin holes or stretched bolt slots is already on its way out. When all these details line up, the result is a concrete fence that stays square, smooth, and consistent from the first pour to the thousandth.
Contact Us
Contact Person: Zhang Zhenlai
Email: [email protected]
Tel/WhatsApp: 8618563210000
Website: https://en.lugongmachinery.com/