Car Air Purifier Factory: A Look at the Production Line Behind Cleaner Cabin Air
2026-09-12
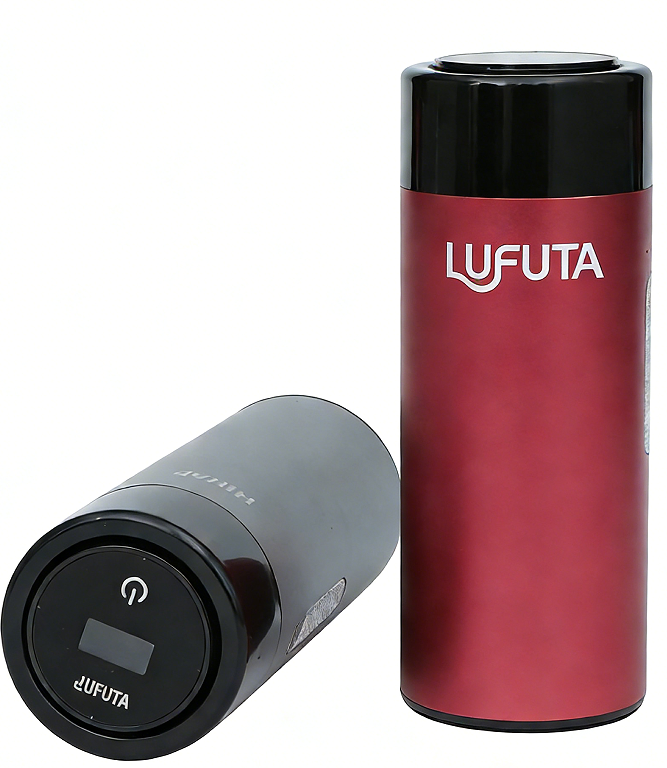
Step inside a car air purifier factory and you’ll quickly realize that cleaner cabin air isn’t a happy accident—it’s built, tested, and refined on a fast-moving production line. At LUFUTATECH, each filter, fan, and housing passes through hands and machines that obsess over what drivers actually breathe. This walkthrough pulls back the curtain on how precision assembly and quality checks turn raw materials into the quiet, dependable purifiers that make every commute a little easier on the lungs.
Melt-Blown Polypropylene Isn't Just Another Layer
A quick glance at a melt-blown sheet might suggest it's just a flimsy white fabric, easy to dismiss as filler. But that impression vanishes the moment you look closer. Unlike the spunbond layers on either side of it, melt-blown polypropylene is engineered with ultra-fine fibers, often a tenth the diameter of a human hair, randomly packed into a dense web. This structure doesn't rely on thickness or stiffness; it works through a labyrinth of microscopic paths that trap particles, droplets, and aerosols. Calling it 'just another layer' misses the entire reason it exists in the first place.
What sets melt-blown material apart is how it does its job. Spunbond gives a mask shape and strength, and a spunbond outer shell repels splashes, but neither can filter the way melt-blown does. The fibers carry a persistent electrostatic charge, which actively pulls in tiny airborne particles that would otherwise slip straight through a woven or knitted fabric. That charge, combined with the tight fiber matrix, creates a filtration performance that mechanical weaving alone can't match. Remove the melt-blown layer, and a mask becomes little more than a breathable decoration with gaps large enough for submicron particles to pass through without slowing down.
In practical terms, melt-blown polypropylene determines whether a respirator actually protects or merely looks the part. The layer's efficiency isn't an accident of material choice; it's the result of controlling polymer melt flow, air temperature, and collector distance to produce fibers with the right diameter and distribution. Manufacturers tweak these parameters to balance breathability and capture rate, because too dense a web makes breathing difficult, while too open a web sacrifices filtration. That balance is delicate, and it's why cheap knockoffs often fail independent testing — their melt-blown layer might look similar but lacks the fiber uniformity or charge stability required for real protection. The next time someone says it's just a layer, remember: it's the layer doing the heavy lifting.
The Cleanroom Step Most Buyers Never See
The cleanroom step most buyers never see isn’t the assembly line or the final inspection—it’s the controlled entry ritual that happens before a single component touches the workspace. Workers pass through an air shower that blasts away loose particles, then don lint-free coveralls, booties, and gloves in a precise sequence. This isn’t bureaucracy; it’s a living barrier against microscopic contamination that can kill a wafer or ruin a batch.
What makes this step invisible is timing. It occurs in a gray zone between receiving raw materials and the first visual check, often during a shift change or while a client is still in the lobby. Buyers might see spotless floors and HEPA filters on a tour, but the real proof is the particle counter trending near zero for weeks after the room is sealed. If that hidden protocol slips, even by a few minutes of rushed gowning, defects can appear months later as unexplained field failures.
A few suppliers now log the entire entry sequence with time-stamped photos or sensor badges, giving buyers a chance to review what they’d otherwise miss. Ask for those records instead of the standard certification report. The cleanest purchase decision comes from knowing what happens in the airlock, not just what the final product looks like on paper.
Why Carbon Pellets Need a Gentler Robotic Hand
Carbon pellets look sturdy, but they carry a hidden fragility that only becomes obvious at the point of contact. A standard industrial gripper, tuned for metal or rigid plastic, often applies pressure that crumbles edges or causes micro fractures. These small breaks aren't always visible at first—yet they quickly change how pellets pack together, how they flow through hoppers, and how they perform in filtration beds. Once the surface texture is roughened, dust starts to appear, and that dust can contaminate downstream processes or throw off precise dosing systems.
A gentler robotic hand changes the equation. Instead of relying on hard jaws and high clamping force, it uses compliant materials and real-time force feedback to hold pellets just firmly enough to move them. The grip adapts to slight variations in size and shape, so each pellet receives even support rather than concentrated stress. That means fewer broken pieces, far less dust, and a more consistent product at the end of the line. For manufacturers, the payoff isn't just lower waste—it's also the confidence that robotic automation won't quietly undermine the very material it's supposed to handle.
The Test Bench That Mimics Bumper-to-Bumper Exhaust
Most emissions labs are content with steady-state numbers, but anyone who has sat in stop-and-go traffic knows that is not the whole story. The bench recreates those exact conditions—idle creep, sudden acceleration, long deceleration—by cycling exhaust gas through a thermal reactor and modulating backpressure on the fly. This lets engineers see how catalysts behave when they never fully reach operating temperature.
Instead of a fixed load curve, the bench uses a programmable valve array and heated sample lines to replicate the heat soak and flow reversals you would get in a real tailpipe. It can push the system from a cold start to full-throttle merge in under 30 seconds, then hold it at a 2 mph crawl for ten minutes. This kind of transient testing catches failures that only appear after hundreds of thermal cycles, like micro-cracks in the substrate or sensor drift.
The result is a much tighter correlation between lab data and on-road behavior. Emission engineers can tune the air-fuel ratio and SCR dosing for conditions that are almost impossible to recreate with a standard dynamometer. It is the difference between passing a regulatory test and actually holding up in real bumper-to-bumper driving, which is what drivers actually care about.
Laser Leak Detection Down to the Micron Level
Pinpointing a leak the width of a human hair used to demand bulky rigs and endless calibration. Modern laser-based systems flip that dynamic by measuring refractive shifts as a gas plume crosses a coherent beam. The result is a positional accuracy down to single-digit microns, even against busy industrial backdrops. Instead of relying on pressure decay or soapy bubbles, operators get real-time coordinate data that points straight to the source.
What makes micron-level laser detection stand out is its immunity to background noise. Traditional acoustic or tracer methods often drown in plant vibrations or ambient hydrocarbons. A focused laser, tuned to specific absorption lines of the target gas, filters out everything but the leak signature. This lets maintenance teams scan flanges, valve stems, and cryogenic seals at a distance, without shutting down the line or scaffolding every joint.
Field results show the practical payoff: a food-grade nitrogen line was losing pressure through a micro-crack invisible to the naked eye. Within six minutes, the laser had mapped a leak path just 4.7 microns wide at the weld toe. Fixing that single point cut waste by 18 percent and eliminated a recurring false alarm from the plant's fixed sensors. That kind of precision turns leak detection from a guess-and-check chore into a surgical repair cue.
How End Cap Seals Prevent Dirty Air From Skipping the Filter
The filter element sits inside a housing, and its end caps are what keep the air path honest. Each cap has a molded lip or gasket surface that presses against the housing when the cover is latched down. This contact creates a continuous barrier around the edge of the media, so incoming air can't simply slip past the sides. If the caps don't seal tightly, even a small gap lets a stream of unfiltered particles ride straight through to the engine.
That tight fit isn't just about initial assembly. Good end cap seals stay slightly compressed while the system runs, absorbing vibration and accommodating minor surface imperfections in the housing. They also resist taking a set over time, which matters because a seal that starts to flatten or harden will gradually open up a bypass route. In practice, the seal turns the filter from a loose cartridge into a closed boundary: every cubic foot of air has to work its way through the media before moving downstream.
FAQ
Engineers begin with a pilot run of about fifty units. They check airflow resistance across the filter media and adjust the fan speed curve so the unit stays quiet under load. Any tweak gets documented before the main line starts.
Most of these purifiers combine a pre-filter for larger debris, a HEPA-grade layer rated around H13, and an activated carbon sheet that handles exhaust gases and volatile organic compounds. The carbon is often impregnated with a catalyst to break down formaldehyde rather than just storing it.
They use a pressure-decay test on each assembled housing. A machine pumps the casing to a set pressure and watches for leakage over several seconds. Units that lose more than a tiny margin are pulled and resealed by hand before retesting.
Cabin filters are passive; they only capture what passes through the HVAC system. An air purifier actively pulls cabin air through denser media and runs even when the fan is low. That gives it a better shot at reducing PM2.5 during stop-and-go traffic, where outside air often gets in through door seals.
Each brushless motor goes through a 72-hour burn-in cycle. The line runs them at slightly above rated voltage while sensors monitor current draw and bearing noise. Early failures get traced back to supplier batches, so a bad lot never reaches final assembly.
Activated carbon saturates over time, so the team bakes incoming carbon to remove residual moisture, then bags it in nitrogen-flushed packaging until it's loaded into filter frames. The final product gets a production date code, and the factory recommends replacing the filter after roughly six to eight months of normal driving.
At the final station, a technician inspects the power button feel and the LED indicator under different light angles. Machines can verify electrical function, but they're not great at catching a button that feels mushy or a lens that catches glare. That tactile pass is still done by hand.
The units sit in molded pulp trays instead of foam. That change cut transit damage noticeably because the tray flexes with vibrations rather than transferring them to the fan housing. Boxes also get a humidity indicator card so distributors can spot storage problems before selling.
Conclusion
On the floor of a car air purifier factory, the melt-blown polypropylene layer isn't just another sheet—it's the first real barrier against fine particulates. Workers and automated lines handle this material with care because its electrostatic charge and fiber density decide how much pollen, brake dust, and soot actually gets trapped. Before any assembly begins, the filter media moves into a cleanroom that most buyers never see. Here, humidity and particle counts are tightly controlled, preventing static discharge or stray fibers from compromising the layer's performance.
Down the line, carbon pellets receive a gentler robotic hand than other components. These activated carbon granules are fragile; a too-aggressive gripper would crush them into dust and ruin their ability to adsorb exhaust gases and VOCs. After assembly, each unit moves to a test bench that simulates bumper-to-bumper traffic, pumping in a cocktail of diesel exhaust and road fumes to verify real-world filtration. Laser leak detection then scans every seam down to the micron level, catching pinholes invisible to the eye. Finally, end cap seals are pressed and checked, making sure dirty air can't skip the filter through the edges. Together these steps turn a plastic housing and layered media into a purifier that actually delivers cleaner cabin air.
Contact Us
Contact Person: Paul Luo
Email: [email protected]
Tel/WhatsApp: 0086-19966314501
Website: https://www.lufutatech.com