Bead Wire Ring Production Line Company Innovations for Stronger Tire Bead Assemblies
2026-10-06
Ask any tire engineer what keeps a tire seated on the rim during hard cornering, and the answer almost always comes back to the bead wire ring. It’s a small component with an outsized job — and for too long, production technology hasn’t kept pace with the demands placed on it. AUGU AUTOMATION is closing that gap. Our latest bead wire ring production line innovations are engineered to produce stronger, more consistent bead assemblies, helping tire manufacturers improve safety, reduce scrap, and stay ahead of increasingly strict performance standards.
Rethinking Bead Ring Geometry for Even Load Distribution
Bead rings rarely fail from a single overload event. More often, small asymmetries in the ring's cross-section gradually shift stress toward one segment of the rim flange. That shift accelerates fretting, loosens the fit, and eventually turns a surface wear problem into a structural one.
Reworking the geometry starts with abandoning the notion that a round wire of constant section is automatically the best load carrier. By tapering the ring's inner face or introducing a slight elliptical crown where the bead seats, the contact patch can be widened without increasing overall mass. The result is a more uniform pressure plume across the seat, rather than a pair of high-stress bands at the edges.
The biggest practical gain shows up under repeated cornering and braking loads. Once the ring no longer digs into the rim at two narrow lines, the seating pressure stays stable longer. That stability also makes assembly less sensitive to minor rim tolerances, which is exactly where many field failures begin.
Precision Winding That Removes Micro-Gaps Between Wires
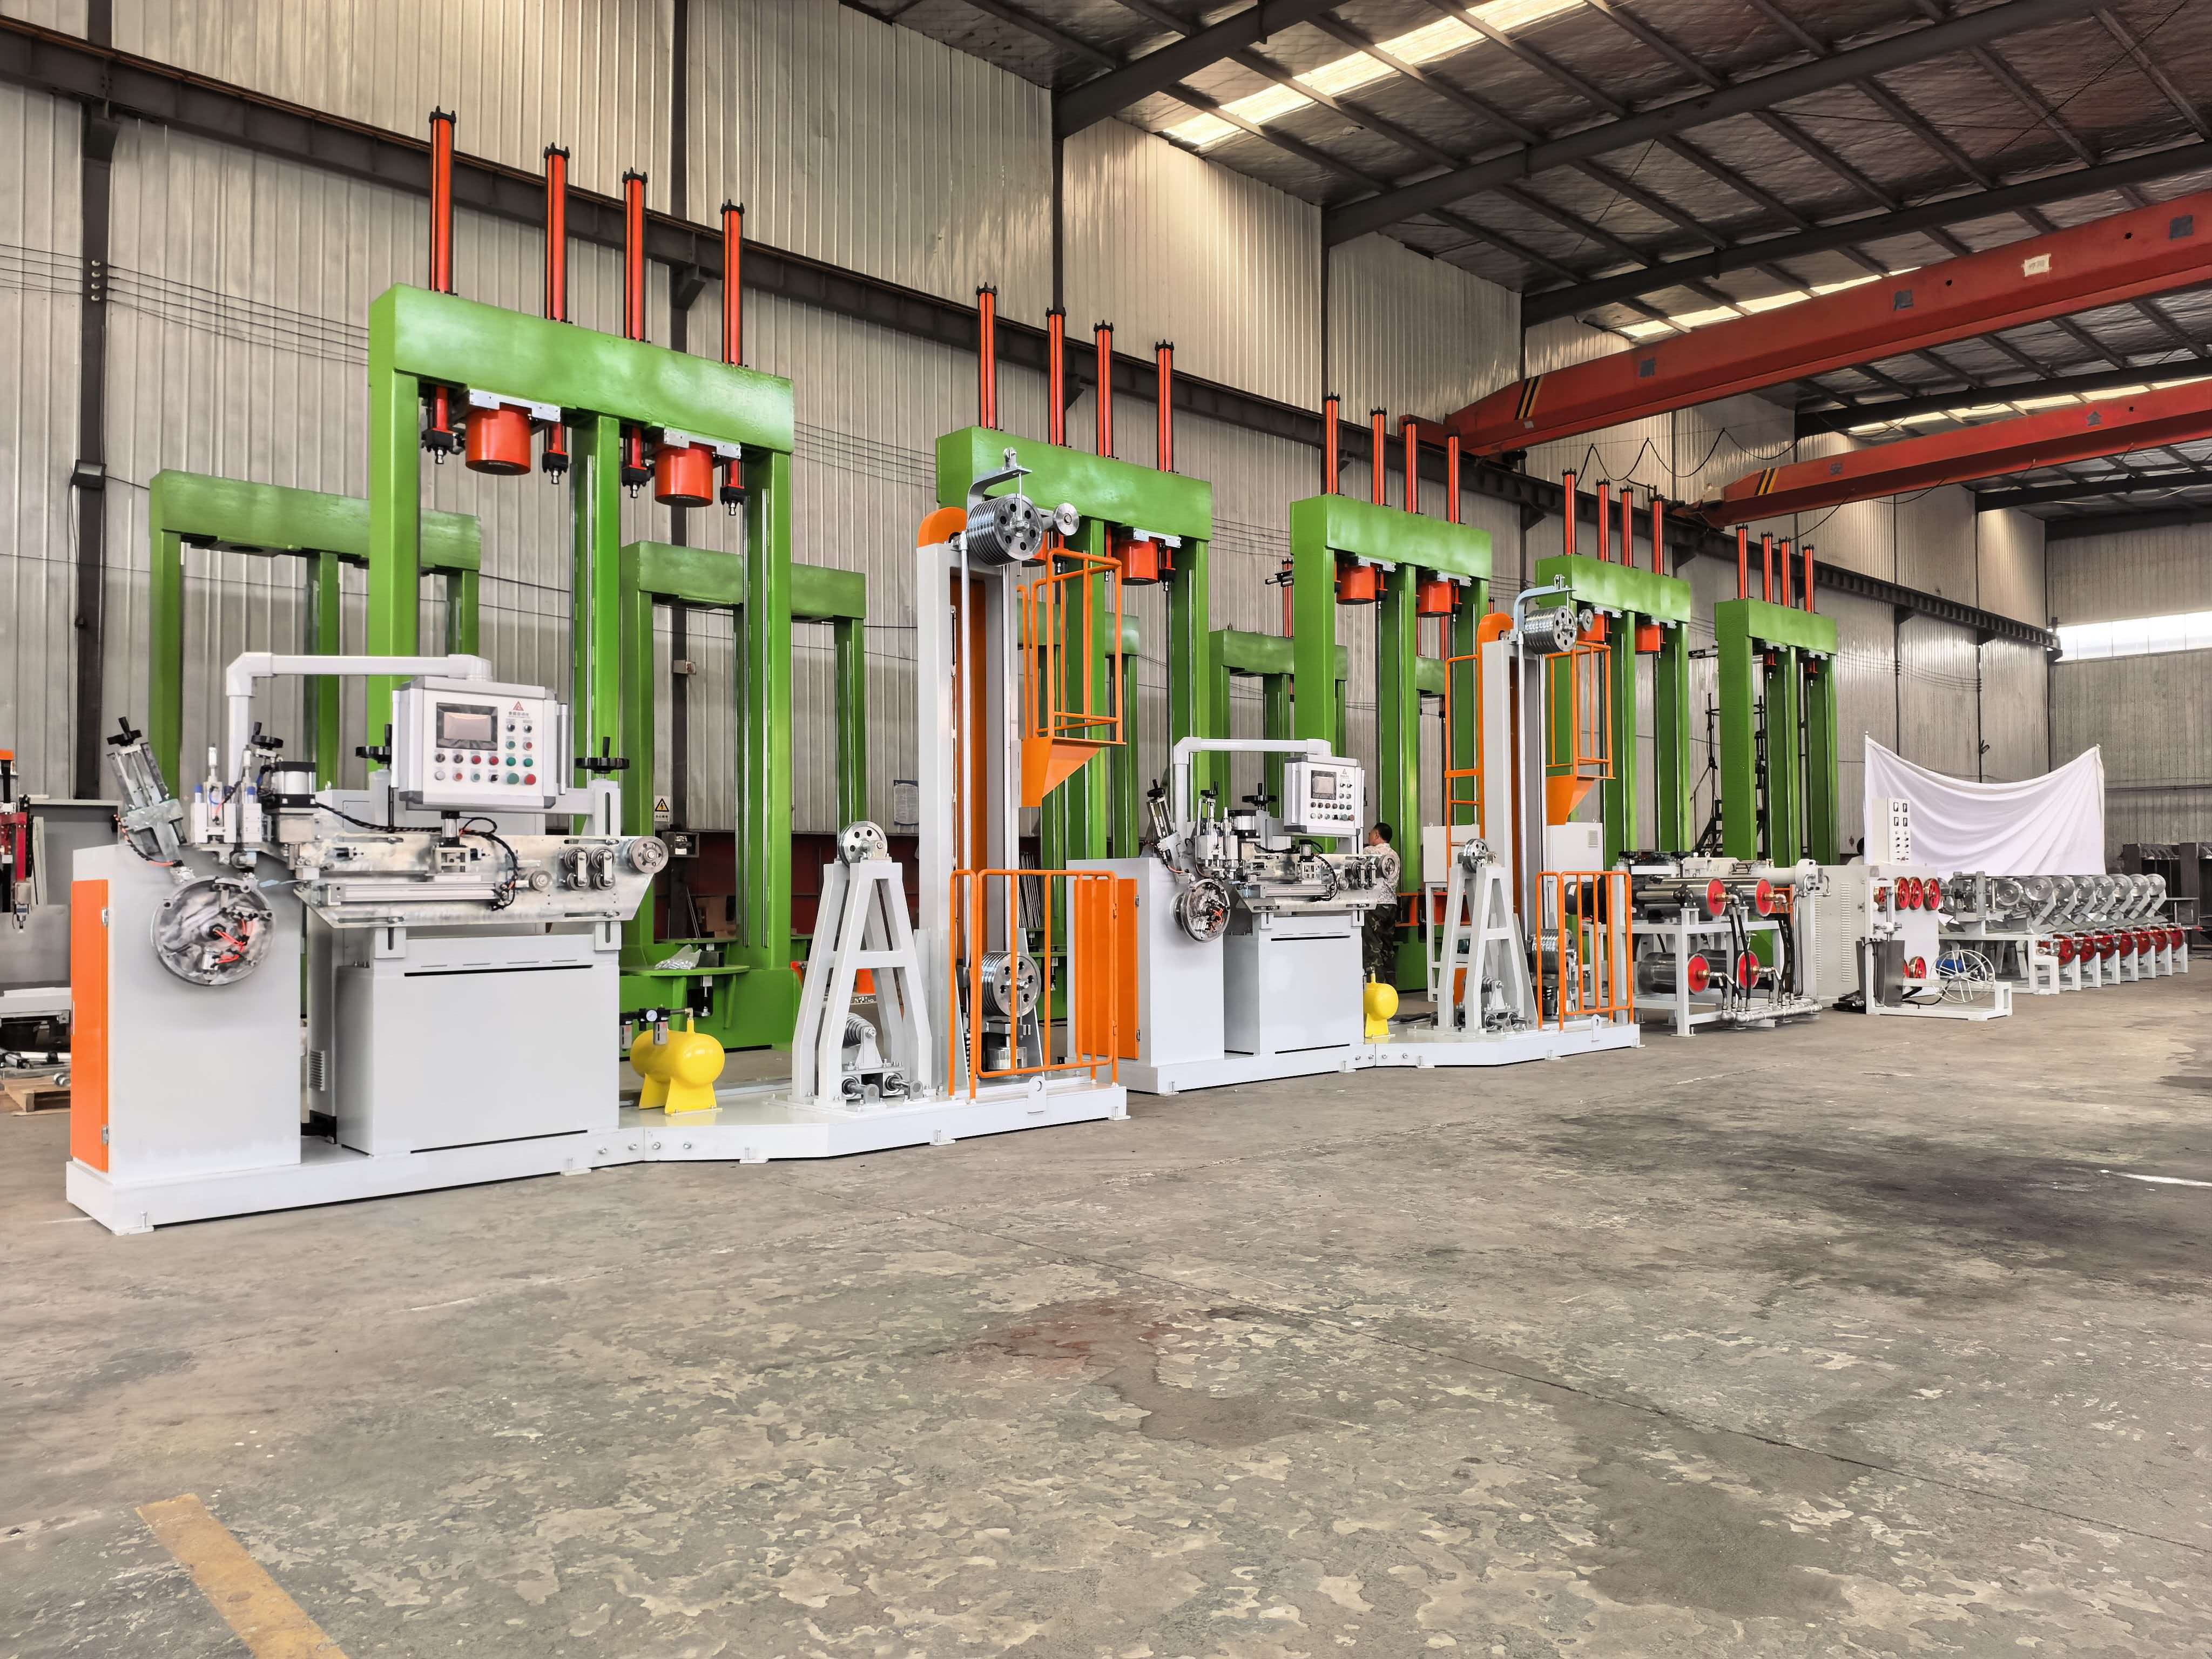
Precision winding eliminates microscopic gaps between adjacent wires by controlling tension, lay angle, and traverse speed within tight tolerances. Unlike conventional winding methods that allow slight irregularities, this approach ensures each turn sits flush against the previous one, resulting in a dense, uniform coil structure.
The removal of micro-gaps directly improves electrical and thermal performance. With no voids between conductors, current distribution becomes more even, reducing localized hotspots and lowering overall resistance. This also enhances heat dissipation, as the tightly packed wires form a continuous thermal path rather than isolated strands separated by insulating air pockets.
In high-frequency and high-power applications, even sub-millimeter gaps can lead to parasitic capacitance and unwanted inductance variations. By achieving a near-solid conductor bundle, precision winding minimizes these parasitic effects, yielding coils with consistent impedance and predictable behavior under load. The result is a component that performs closer to its theoretical ideal, with fewer manufacturing-induced deviations.
Surface Treatments That Turn Ordinary Wire Into Bond-Ready Steel
Raw steel wire straight off the drawing line rarely bonds well to adhesives, rubber, or paint. Mill scale, drawing lubricants like calcium stearate, and a thin oxide skin all sit on the surface, forming a weak boundary layer that lets coatings peel away under load. The first job of any bond-enhancing treatment is to strip that layer without etching the underlying steel too aggressively. A controlled acid pickle followed by an alkaline rinse removes most organic residue, but it often leaves the surface too smooth for mechanical anchoring. That is where the next step comes in.
Grit blasting with fine aluminum oxide or steel shot creates a random micro-roughness that increases the real contact area several times over. For wire that must bond to rubber in tire bead or hose reinforcement, a zinc phosphate conversion coating works even better: it grows a crystalline layer with microscopic pores that act like tiny mechanical locks while also protecting against flash rust. In high-spec applications, a thin silane primer or low-pressure plasma treatment replaces older solvent-based primers. These methods leave behind reactive hydroxyl or amine groups that covalently bond with epoxy, polyurethane, or RFL dips, so the interface becomes stronger than the coating itself.
Inline Vision Systems That Catch Weak Points Before Assembly
Weak points rarely announce themselves. A hairline crack in a die-cast bracket, a slightly off-center drilled bore, or a surface fold in stamped sheet metal can sail through upstream processes and only become obvious when parts refuse to mate on the final line. Inline vision systems change that equation. Mounted directly over the conveyor or robot transfer point, they photograph or scan each component before it reaches the next station and compare what they see against CAD tolerances, surface models, and historical defect libraries. The result is an early, automatic flag—often within milliseconds—so questionable parts never make it into an assembly.
The real power of these systems isn't just the camera; it's the decision logic tied to the line. High-speed imagers catch sub-millimeter deviations, while structured light or laser profilers map contours that 2D photos miss. When a weak point is detected, the software can trigger a soft eject, mark the part with ink, or simply pause the feeder and alert an operator with a saved image and measured deviation. This turns the inspection station into a feedback loop: batch trends become visible before they turn into rework piles, and suppliers get concrete evidence instead of vague complaints.
Inline inspection also reshapes how engineers think about yield. Instead of relying on downstream torque tests or leak checks to reveal assembly problems, they can stop the weak point at its source. For high-mix lines, quick recipe changes let one vision setup handle multiple part numbers without dedicated gauging fixtures. The payoff shows up in fewer line stoppages, lower scrap, and a final assembly that no longer has to compensate for parts that were almost good enough.
Modular Tooling for Low-Profile and Heavy-Duty Tire Lines
Tire manufacturing demands tooling that can keep pace with the divergent requirements of low-profile and heavy-duty lines. Low-profile tires push limits on sidewall stiffness and tread precision, while heavy-duty variants impose extreme stress on forming and curing equipment. Modular tooling addresses both by breaking down critical components into interchangeable segments—clamps, bead rings, and tread segments can be swapped or adjusted without replacing entire assemblies. This design philosophy reduces changeover times and lets a single line produce both tire types without sacrificing dimensional accuracy or surface quality.
Beyond flexibility, modular systems bring tangible gains in durability and maintenance. In heavy-duty production, tools face repeated thermal cycling and high clamping forces, so wear-prone areas are engineered as separate, easily replaceable modules. For low-profile tires, precision indexing features ensure consistent sidewall contouring even at tight aspect ratios. The result is a tooling strategy that lowers long-term capital expenditure, minimizes downtime, and keeps quality metrics stable across a wider product mix.
Cooler Welding Methods That Preserve Wire Strength
Wire strength drops quickly when a weld zone gets hot enough to trigger grain growth or annealing. Cooler welding methods sidestep this by limiting the heat-affected zone. Capacitor discharge welding, for instance, dumps a high-current pulse in milliseconds. That fuses the joint before surrounding wire reaches a temperature that would undo prior cold working or tempering.
Ultrasonic welding takes an even lower-temperature route. It uses high-frequency vibration to scrub oxides off the mating surfaces and create a solid-state bond, so the wire never melts. Cold pressure welding works on a similar principle, forcing clean metal surfaces together under high pressure until they share electrons. Both methods leave the base wire's tensile strength largely intact.
Pulsed MIG and TIG setups can also run cool when tuned properly. Short, spaced-out pulses let heat dissipate between cycles, and using a lower background current keeps the overall heat input down. For wire products, adding a quick tensile test on sample joints is the simplest way to confirm the chosen method isn't quietly degrading the material.
FAQ
It delivers the repeatable geometry and surface finish that a tire bead needs to lock securely onto the rim. Without that consistency, bead assemblies can show uneven seating, pressure loss, or premature fatigue under cornering loads.
Newer lines use closed-loop tension control and laser-based diameter checks during winding. These catch small deviations before the ring is cured into the tire, reducing micro-cracks and residual stress that weaken the bead over time.
Heavy-duty applications demand thicker wire and higher tensile strength, which makes bending and joining more difficult. Older equipment can introduce flat spots or weld embrittlement, so many upgrades focus on servo-driven forming heads and staged cooling after welding.
Yes, modern systems often use adjustable forming mandrels and recipe-based parameter sets. An operator can switch from a passenger car diameter to a light truck diameter in minutes, with automatic recalibration of tension, speed, and splice position.
Tension variation creates internal stress gradients in the steel wire. During high-speed driving or hard braking, those gradients can turn into fatigue cracks near the weld or along the winding path, so real-time feedback keeps tension within a narrow band.
Automated vision systems inspect surface defects, diameter, and weld integrity at multiple stations. Instead of waiting for batch testing, the line can reject a single faulty ring immediately and adjust parameters before more bad parts are produced.
Electric vehicles deliver instant torque, placing greater stress on the tire bead during acceleration and regenerative braking. Production lines now include pre-deformation control and adhesion monitoring to create a denser, more uniform bead that resists rim slip.
Predictive maintenance is becoming common, with sensors tracking bearing temperature, vibration, and motor current. Combining that data with routine checks of forming dies and splice tooling helps avoid unplanned downtime and keeps ring quality consistent.
Conclusion
A bead wire ring production line company has rebuilt its approach from the ground up, starting with the ring geometry itself. Rather than sticking to conventional circular profiles, engineers now map stress distribution across the bead under simulated tire inflation and cornering loads, then adjust the cross-section and curvature so that force is spread evenly instead of concentrating at a handful of contact points. This geometry work is paired with precision winding stations that use individually controlled tension arms and closed-loop feedback to pull each wire into exact alignment, eliminating the microscopic gaps that previously allowed rubber to creep in and weaken the bond. Once wound, the wire passes through a surface treatment stage designed to strip away drawing lubricants and oxide layers, then deposit a thin, chemically active coating that primes the steel for adhesion without adding brittle intermetallic layers.
Down the line, inline vision systems inspect every ring before it reaches the tire building drum. Multiple cameras and laser profilers measure wire spacing, ring roundness, and weld collar dimensions, flagging any deviation that could become a fatigue crack under repeated flexing. The company has also moved to modular tooling, so the same production cell can switch between low-profile passenger tire beads and heavy-duty truck beads by swapping mandrel segments and guide rollers rather than retooling an entire line. For the welding operation, cooler methods such as pulsed resistance welding with rapid post-weld quenching preserve the original wire tensile strength, avoiding the soft zones that often appear next to a traditional weld. Taken together, these changes produce bead rings that hold their shape under overload, resist corrosion at the wire-rubber interface, and extend the service life of the finished tire without adding unnecessary weight.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/