Anodizing Equipment Supplier: Essential Considerations for Selecting the Right Partner
2026-10-09
Choosing the right anodizing equipment supplier can make or break your production quality and efficiency. From tank design to power delivery, every detail matters—yet many buyers overlook the long-term support that separates a one-time vendor from a true partner. At Junda, we’ve seen how hidden engineering choices impact everything from coating uniformity to energy costs. In this guide, we’ll walk you through the essential factors that go beyond a glossy brochure, helping you avoid costly missteps and find a supplier who actually understands your line’s unique demands.
Ask for Real Production Data, Not Just Benchmark Numbers
Synthetic benchmarks tend to paint a rosy picture because they run in a controlled environment with predictable traffic patterns. Once your service handles real users, the story changes. Memory leaks that never appeared in a five-minute load test suddenly show up after six hours of sustained traffic. Garbage collection pauses that look fine on a graph become the reason your p99 latency spikes every Tuesday at 3 a.m.
Ask the vendor or internal team for production metrics pulled from their monitoring dashboards, not a sanitized summary. Real data includes incident timelines, crash dumps, and resource usage during a traffic surge. Those numbers reveal how the system behaves when a database connection pool saturates or a background job queue backs up—things no benchmark suite bothers to simulate.
You also want to see the ugly parts: failed deployments, rollback frequency, and the mean time to recover from a partial outage. A system that scores high on a throughput benchmark but has never survived a region failover will cost you more in the long run than one with lower raw numbers and a proven track record under real load.
Inspect the Wetted Materials for Long-Term Acid Resistance
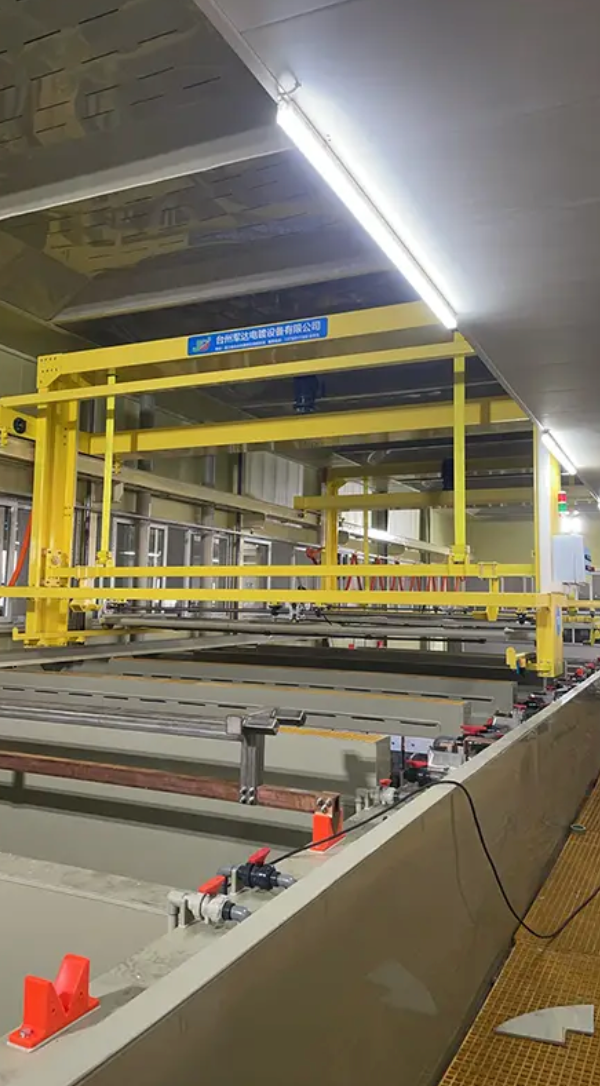
Before committing any vessel, pipe, or lining to continuous acid service, pull the wetted parts list and verify each material against the actual acid concentration, temperature range, and expected contact duration. A material that survives a 24-hour spot test can still degrade after months of exposure through slow leaching of plasticizers, stress cracking at fittings, or gradual surface erosion from minor flow turbulence. Check seals, gaskets, and valve seats just as carefully as the main body—those soft goods often fail first and are the least documented in typical corrosion charts.
Long-term acid resistance is not a single property but a combination of chemical inertness, hydrolytic stability, and resistance to micro-cracking under intermittent wet/dry cycles. For polymers, look for evidence of swelling, discoloration, or loss of flexibility in previously submerged sections. For metals, inspect weld zones and crevices for pitting or preferential attack, since stagnant acid trapped in a thread or behind a flange can concentrate over time even when the bulk solution remains mild. Pull a few sacrificial samples and section them if possible—surface appearance often hides internal degradation.
If your application involves temperature swings or periodic cleaning with different chemicals, cross-check compatibility under those transient conditions as well. An acid-resistant liner may fail when exposed to hot rinse water or alkaline detergent between batches. Record any signs of haze, roughness, or dimensional change during routine maintenance, and compare them against baseline measurements taken at installation. Small changes in surface texture can indicate that the material is nearing the end of its useful life, even if it still holds pressure today.
See How Easily the Control Panel Adapts to New Part Geometries
The moment you load a new part file, the control panel doesn't sit there waiting for manual tweaks. It reads the geometry directly—whether that's a deep pocket, a thin wall, or an odd contour—and reshuffles its own layout on the fly. Toolpaths, spindle speeds, and feed rates adjust themselves before you even think to reach for a dial.
That same panel handles the switch from a simple rectangular block to a curved aerospace bracket without a single line of new code. You simply drag the part into place, hit the scan, and watch as the interface repopulates with only the relevant controls. Nothing extra, nothing missing—just the exact buttons and readouts that match the shape in front of you.
Because the panel learns geometry instead of forcing you to translate it, setup time drops from hours to minutes. Operators stop memorizing layer after layer of menus and start trusting the screen to keep up with whatever part comes next.
Demand Clarity on Agitation and Temperature Uniformity
Uneven mixing rarely announces itself until the batch is already off-spec. That's why we push for a plain, measurable answer on how agitation energy gets distributed across the vessel and how heat travels through the load — not just the setpoint on a controller.
The real test isn't a single probe reading near the wall or a smooth curve on a datasheet. It's whether the center, corners, and surface stay within a tight band when viscosity shifts, fill level changes, or a cycle pauses. Without that, any recipe is just a hope.
Look for a Supplier Who Trains Your Team on Maintenance and Safety
A supplier that actually sticks around after the install to walk your crew through routine upkeep and emergency stops is rare. Ask for a training session that happens on your floor, with your equipment, not in a conference room. If they can’t point out the grease fittings, wear points, and the exact lockout procedure for the machine they just sold you, that’s a red flag.
Maintenance training shouldn’t end with a binder full of laminated sheets. The best suppliers offer short follow-up visits or video calls after a few weeks, once your team has had time to use the equipment and run into real questions. They should also cover safety scenarios specific to your workflow, like clearing a jam or responding to an overload alarm, rather than reading off generic safety checklists.
A practical way to test this is to ask for a sample training outline before you sign. If it lists the model numbers of your machines and includes timed, hands-on checks, the supplier has done this more than once. If it’s just a slide deck about best practices, keep looking.
Factor in Energy, Chemical, and Replacement Costs Over a Decade
Most people compare purchase prices and stop there. That misses where the real money goes. A system with a lower upfront tag can quietly drain your budget through higher electricity draw, more frequent chemical dosing, or parts that fail just after the warranty expires. Spread those differences across ten years and the gap becomes impossible to ignore.
Energy use is rarely constant—it shifts with load, weather, and maintenance habits. A unit that runs efficiently at half load might guzzle power when ambient temperatures climb or filters clog. Chemical consumption follows a similar pattern: cheaper designs often need more additives to hit the same output quality, and those additives get pricier every year. Then there are replacement parts. Pumps, seals, sensors, membranes—each one carries a hidden schedule. Without tracking actual failure rates, you're guessing.
The smart approach is to build a simple decade-long model. Take today's energy rate, add a conservative annual increase, and multiply by expected runtime hours. Do the same for chemicals using real dosing data, not spec sheets. For replacements, dig into service records or talk to operators who've run the equipment past year three. You'll often find that a 15% higher initial cost pays for itself two or three times over before the decade ends.
FAQ
Look beyond the number of years in business. Request case studies or references from facilities that run similar processes—whether that's Type II sulfuric anodizing, Type III hardcoat, or chromic acid. A supplier who has actually dealt with your alloy mix and production volume will understand nuances like tank sizing, agitation, and rectifier ripple.
It's critical. Off-the-shelf systems rarely match real-world layout constraints or throughput targets. A good partner will assess your floor space, power availability, waste treatment setup, and future expansion plans before proposing tank dimensions, automation level, and rectifier capacity. They should be able to explain why a certain configuration fits your operation instead of pushing a standard package.
Ask about response times for breakdowns, availability of spare parts, and whether they offer remote diagnostics or on-site training for your maintenance crew. Also clarify if they have process engineers who can help troubleshoot coating defects like burning, pitting, or uneven film thickness—because equipment alone won't solve every finishing problem.
Check materials and fabrication details. Tanks should be constructed from suitable plastics like polypropylene or PVDF with proper welding, not just glued seams. Rectifiers need low ripple (ideally under 5%) for consistent anodizing, and cooling systems must be sized for continuous duty. Ask about warranty terms on major components and whether they use proven brands for pumps, heaters, and controls.
Because downtime in an anodizing line can quickly erase any upfront savings. A cheaper system that lacks local service support or has long lead times for replacement parts can leave you stranded for weeks. Factor in the cost of lost production, rushed shipping, and potential rework when comparing quotes—not just the equipment price tag.
The best suppliers act as consultants, not just vendors. They should understand how factors like bath chemistry, temperature control, and current density interact. If they can't discuss topics like aluminum dissolution rates, sealing methods, or rectifier ramp profiles, they may not be able to help you achieve consistent, specification-compliant finishes.
Ask for documentation on ventilation design, acid mist suppression, and waste treatment integration. A responsible supplier will incorporate features like fume extraction, spill containment, and secondary containment for chemical storage. They should also be familiar with local codes for electrical safety in wet environments and help you plan for compliance from day one.
Create a weighted scoring matrix that includes not just capital cost, but also energy efficiency, automation level, service network, lead time, and references. Visit an existing installation if possible—seeing how the line performs after a year or two of real production tells you more than a polished brochure. Also ask about upgrade paths; a system that can grow with your business is worth more than a static setup.
Conclusion
A credible anodizing equipment supplier seldom leads with a glossy catalogue or one perfect lab test. Ask instead for production logs from actual lines—voltage drift, bath temperature swings, and shutdown records reveal more than any benchmark sheet. While you are there, inspect every wetted part: tanks, heat exchangers, pump housings, and seals all need demonstrated resistance to hot acid, not just a material certificate. And pay close attention to how easily the control panel adjusts when a new part geometry arrives. If recipe changes require a vendor service call or a custom software patch, the line will idle every time your product mix shifts. Reliable partners welcome that scrutiny instead of deflecting it.
On the process side, demand clear answers about agitation flow and temperature uniformity across the tank; even a few degrees of variance or an uneven circulation pattern produces blotchy finishes and rejected loads. The right partner will also train your operators and maintenance team properly—covering acid handling, ventilation checks, and emergency shutdowns—rather than leaving a manual and walking away. Last, calculate ownership over ten years: rectifier and chiller energy use, chemical replenishment rates, and expected replacement of pumps, anodes, and seals. If a supplier avoids those figures, assume the real operating cost is higher than the quote suggests. That unspoken gap often determines whether the line stays profitable after the warranty period.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com