3D Car Floor Mats Factory Reveals How Precision Molding Creates All-Weather Protection
2026-10-19
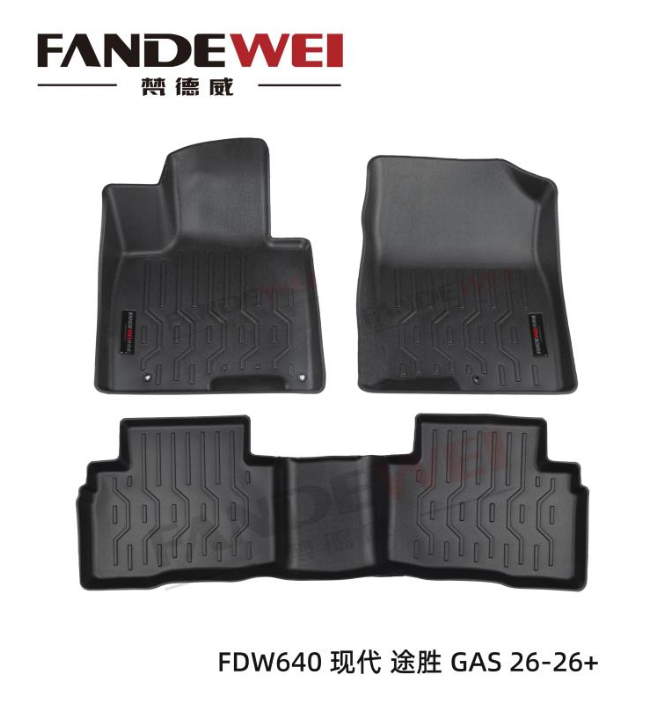
Ever wondered what separates a flimsy floor mat from one that laughs off mud, snow, and spilled coffee? Inside a 3D car floor mats factory, precision molding isn’t just a buzzword—it’s the reason every contour locks into place and every edge stays put through the messiest seasons. At FANDEWEI, that obsession with exact fit and all-weather durability starts long before the first layer is poured. Here’s a look at how the process unfolds, and why your car’s interior deserves the upgrade.
The Molding Machine That Turns Polymer Pellets into a Perfect Fit
A hopper full of raw polymer pellets looks unremarkable, but inside this machine those tiny beads undergo a transformation that borders on alchemy. Heated to a precise viscosity, the melted plastic is forced through a gate into a cavity machined to tolerances thinner than a human hair. The result is a component that slips into its mating part with no slop, no binding, just a quiet click.
The real trick isn't just melting and injecting - it's controlling pressure, temperature, and cooling rate so the polymer chains align in ways that minimize warpage. Every mold is a bespoke puzzle, designed to anticipate how the material will shrink and settle. That's why each cycle produces parts that don't need hand-finishing; they come out ready to assemble.
Operators quickly learn that the machine's feedback loop is relentless. Sensors track viscosity in real time, adjusting injection speed on the fly. If a batch of pellets arrives slightly denser from the supplier, the machine compensates without being told. That is what separates a molding machine from a perfect fit maker - it doesn't just shape plastic, it negotiates with it.
Why a 3D Scan Is the First Step to All-Weather Defense
Most off-the-shelf covers rely on generic vehicle profiles that ignore the small details—mirror stalks, roof rails, spoiler lip. A 3D scan records those exact shapes, down to a few millimeters, so the protective layer that comes later can hug every curve instead of leaving pockets where water pools or wind gets underneath.
The value of scanning shows up most during harsh weather. When rain hits at highway speed or ice forms overnight, any looseness in a cover turns into a tear point. With scan data, you can pre-position seams and tension zones where they actually belong, so the finished product sheds water and snow rather than catching it.
Scanning also gives you a repeatable baseline. Attach a new rack, swap mirrors, or notice a panel has shifted slightly and a fresh scan picks up those changes before the old fit becomes a liability. That keeps the all-weather protection working as intended, year after year.
The Material Formula That Repels Water, Mud, and Salt
Most surface treatments fail the moment real-world grime gets involved. This formula takes a different route by altering the substrate at a molecular level, creating a barrier that doesn't just sit on top but becomes part of the material itself. The result is a surface where water beads up and rolls away before it can even think about leaving a mark, while mud and salt simply can't find a grip.
What sets this approach apart is how it handles salt specifically. Road salt, ocean spray, and industrial residue are notoriously corrosive, eating away at unprotected surfaces within weeks. By repelling the saline solution at the point of contact, the formula stops the electrochemical reaction that leads to rust and pitting. This isn't a temporary coating that washes off; it's a permanent shift in how the material responds to aggressive environments.
Field testing in coastal and winter maintenance settings shows a consistent pattern: surfaces treated with this formula stay cleaner longer and require far less aggressive cleaning when maintenance is needed. Mud that would normally bond and harden simply sloughs off with a light rinse. For anyone dealing with vehicles, outdoor equipment, or architectural surfaces exposed to the elements, that means less downtime and a longer functional lifespan.
How High-Pressure Molding Seals Every Edge Against Leaks
The core advantage of high-pressure molding lies in its ability to force material into every microscopic crevice along a component's boundary. Unlike conventional assembly methods that rely on gaskets or adhesives applied after the fact, this process injects the sealant or substrate at pressures exceeding 3,000 psi. That intense force pushes the material not just against the visible edge but into the tiny irregularities, voids, and tooling marks that would otherwise become leak paths under thermal cycling or vibration.
A closer look at the molding cycle reveals why no edge escapes coverage. During the injection phase, the mold cavity is held shut under clamping tonnage calculated to resist the internal pressure. As the molten compound rushes in, it fills the runner system and then hits the part perimeter with enough velocity to achieve what engineers call "edge packing." This is not a surface coating—it is a volumetric saturation of the boundary zone. Even sharp corners, thin flanges, and undercuts that frustrate post-applied seals are completely enveloped because the material is still in a fluid state and driven by pressure differentials, not manual placement.
The result is a monolithic, leak-proof envelope that performs consistently over the product's life. There are no seams where two separately manufactured seals might separate, no adhesive layer that can degrade or peel, and no opportunity for assembly misalignment. High-pressure molding turns the entire edge into a continuous, stressed-against-the-substrate barrier. For applications ranging from automotive electrical connectors to industrial sensor housings, that means fewer warranty claims, better IP ratings, and a seal that survives where traditional methods fail.
A Mat's Journey from Digital Design to the Factory Floor
It starts on a screen, where a designer nudges vectors and tweaks curves until the mat's silhouette feels just right. Texture samples get dragged across the digital surface, thickness parameters are dialed in, and a quick render shows how light falls across the ribbed pattern. Nothing is physical yet, but every decision is already shaping how the mat will eventually feel underfoot.
Moving from pixels to production means handing the file to engineers who care about draft angles and material shrinkage. A first prototype gets cut from a block of foam, then pressed and flexed until weak spots show up. The digital model returns to the screen for a round of quiet adjustments: a slightly deeper groove here, a firmer edge there. When a second prototype survives the drop test and the abrasion wheel, the design finally earns its place on the factory schedule.
On the factory floor, the mat's journey becomes loud and mechanical. Rolls of rubber feed into a cutter that follows the original design paths, stamping out shape after shape. Conveyors carry the blanks through heat presses that fuse the surface texture, while workers at the end of the line check for bubbles and uneven edges. A final trim, a quick logo stamp, and the mat is rolled, bagged, and ready to be shipped, no longer a collection of digital points but something you can stand on.
How the Factory Tests Mats in Simulated Downpours and Snow
Inside a sealed chamber at the back of the plant, water cannons mounted on a rotating gantry fire a steady wall of spray at a floor mat pinned to a steel incline. The nozzles are set to mimic a tropical downpour—roughly two inches of rain per hour, hitting at a 30-degree angle. Technicians watch through polycarbonate windows as the mat's surface turns from dark gray to near-black with saturation. They're not looking for total waterproofing; they want to see how long it takes for water to bead off the high-traffic zones versus soaking into the edges. After twenty minutes, the mat is flipped over and a moisture sensor is pressed against the backing. If the reading crawls above a set threshold, the batch gets flagged for extra drainage channels.
Snow testing happens in a walk-in freezer the size of a shipping container, kept at minus twelve Celsius. A fine mist machine—originally designed for ski slope grooming—lays down a two-centimeter layer of artificial snow over the mat's surface. Then a worker sprinkles a measured amount of rock salt across the top, the same stuff that gets tracked in from icy sidewalks. The real challenge comes when the freezer door opens and room-temperature air rushes in. The snow turns to slush within minutes, and that's when the mat's fiber density matters. A good mat should hold the meltwater in its upper layer long enough for it to evaporate, not let it pool underneath and freeze into a slick patch overnight.
The data from both chambers feeds into a single spreadsheet that gets reviewed every Friday. If a particular mat soaks up rain but fails the snow-melt test, the compounding team might swap out five percent of the polypropylene for a coarser denier, or add more rubber nibs to the underside. One trick the testers learned from a Scandinavian client: sprinkle a pinch of fine silica sand before the rain test, because that's what actually ends up in the grooves after a week of use. Without it, the water flow numbers look artificially clean.
FAQ
They're shaped using precision scans of the vehicle floor, so every contour, including around seat rails and center humps, is captured. That means no bunching or sliding, just a tight, glove-like fit.
The factory starts with digital vehicle data, then uses heated sheets of durable polymer that are vacuum-formed over a custom mold. After cooling, edges are trimmed with CNC cutters to match the exact footwell dimensions.
Most high-quality 3D mats use a layered TPE or XPE core with a textured top skin. These materials stay flexible in freezing temperatures, resist cracking, and can be rinsed clean without absorbing water.
They're designed for year-round use. The raised edges trap melted snow, mud, and rain, but they also keep sand and dust from grinding into the carpet during summer. The UV-stable surface doesn't warp or fade in heat.
Each design includes clearance zones around the accelerator, brake, and clutch. Prototypes are test-fitted in real vehicles, and any mat that shifts under load or sits too close to a pedal is reworked before production.
Yes, because the mats have a continuous raised lip around the perimeter, usually 2 to 3 centimeters high. That creates a tray-like barrier, so liquids pool on the surface until you pour them out.
Check the edges for clean, uniform trimming and look at the underside—real precision mats often have a non-slip backing and clips that match factory anchor points. Cheap copies tend to have wavy edges and stiff, plastic-smelling material.
With normal cleaning, a well-made 3D mat can last five to eight years or more. The key is avoiding harsh solvents that can dry out the top layer, and occasionally removing them to let the underlying carpet breathe.
Conclusion
Inside a 3D car floor mat factory, precision molding starts long before polymer pellets enter the machine. Technicians begin with a laser scan of the vehicle's footwell, capturing every contour and anchor point. That digital map drives the entire process—no universal template, just a fit shaped to the exact floor. The molding machine then heats and injects a custom material blend, one engineered to shrug off water, mud, and road salt without cracking in freezing temperatures. High-pressure molding forces the compound into every corner and along raised edges, forming a sealed lip that keeps slush from leaking onto the carpet underneath. It's a method built on tight tolerances, not guesswork.
From that digital design, the mat moves to the factory floor where each batch is tested under simulated downpours and packed snow. Workers check for buckling, edge lift, and seepage. Each test cycle repeats with rapid temperature shifts to expose weak seams before a single mat ships. The material formula is adjusted by season and climate, but the goal stays the same: all-weather defense that holds up after years of abuse. The result is a mat that looks simple but reflects a chain of precise steps—scanning, compounding, high-pressure molding, and real-world abuse testing. That is how a factory turns raw polymer and a 3D scan into protection you don't think about until the next storm hits.
Contact Us
Contact Person: Jet
Email: [email protected]
Tel/WhatsApp: 8619903745266
Website: https://www.fandewei.com/